Fiber Laser vs CO2 Laser: Cutting, Engraving & Costs
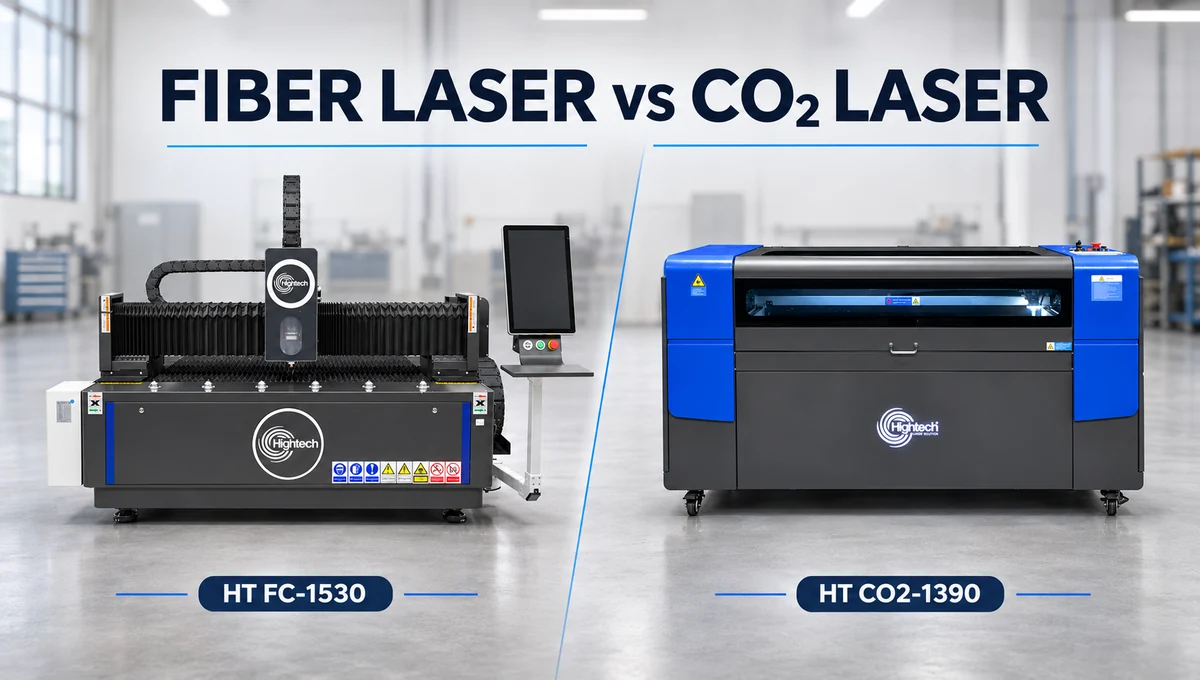
Table of Contents
Choosing between a fiber laser and a CO2 laser is not simply a question of which technology is newer or more powerful. The correct choice depends on the materials you process, the quality your customers expect, your production volume, and the jobs you want to add to your business.
Fiber lasers are optimized for metal. They are widely used for stainless steel, mild steel, aluminum, brass, copper, titanium, and other metal applications where speed, narrow kerfs, consistent detail, and low optical maintenance are important. CO2 lasers are strongest on non-metal materials such as acrylic, wood, MDF, leather, fabric, paper, and selected plastics. They remain a practical choice for sign shops and mixed-material workshops that depend on clean acrylic edges and detailed engraving.
For many companies, the decision is therefore not “Which laser is better?” but “Which laser matches the work that generates most of our revenue?” This guide compares fiber and CO2 systems for industrial metal cutting, signage, material quality, maintenance, operating cost, and return on investment.
Quick answer
Choose a fiber laser when most of your work involves metal, especially thin and medium-gauge sheet, reflective metals, metal letters, plaques, components, or high-volume production. Choose a CO2 laser when most of your work involves acrylic, wood, MDF, fabric, paper, or other non-metals. A sign shop with a balanced mix of metal and non-metal work may eventually need both technologies.
Two distinctions matter: industrial CO2 systems can cut metal when designed for that purpose, and a fiber marking machine is different from a fiber sheet-cutting machine. Match both the laser technology and the machine configuration to the job.
Fiber Laser vs CO2 Laser: Technical Comparison
The main differences are the laser source, wavelength, material response, and beam-delivery system. The comparison below describes common industrial cutting and workshop engraving applications; individual machine capabilities still need confirmation.
Factor | Fiber Laser | CO2 Laser |
|---|---|---|
Typical wavelength | About 1.06–1.07 µm for common industrial systems | About 10.6 µm; other wavelengths also exist |
Laser source | Solid-state, using doped optical fiber | Electrically excited gas mixture |
Best material match | Metal cutting and marking; selected plastic marking | Acrylic, wood and other compatible non-metals |
Beam delivery | Fiber-optic delivery to the processing head | Usually a mirror-and-lens beam path |
Reflective metals | Well suited when the system is approved for the material | More challenging; not a routine application for workshop CO2 machines |
Acrylic cutting | Not a practical substitute for a CO2 acrylic cutter | Suitable for cutting; edge finish depends on acrylic type and settings |
Metal cutting speed | Often faster on thin and medium sheet | Industrial systems can cut metal, but productivity depends on the application |
Typical buyer | Metal fabricator or metal-sign producer | Sign shop, engraving business or mixed non-metal workshop |
Optical maintenance | Less beam-path alignment; cutting-head optics still need care | Mirrors and optics require inspection, cleaning, and alignment as specified |
Is a “CO2 Fiber Laser” a Single Laser Type?
CO2 lasers and fiber lasers are two different laser technologies. CO2 lasers use a gas-based source, while fiber lasers generate and amplify light in doped optical fiber. A machine advertised with both technologies needs separate sources and a suitable design for each process; one source does not change into the other.
Why Wavelength Changes Material Performance
The most important difference between fiber and CO2 lasers is wavelength. Many metals absorb the shorter wavelength of a fiber laser more effectively than the CO2 wavelength, while many organic and non-metal materials respond well to the longer CO2 wavelength. Absorption also depends on material composition, surface condition, and temperature.
Fiber Laser: Short Wavelength for Metal Absorption
Common industrial fiber cutting systems operate near 1.06–1.07 µm. Their wavelength and beam characteristics support efficient metal processing, but do not guarantee a particular tolerance, cutting thickness, or finish. The source, optics, motion system, assist gas, and parameters must work together.
CO2 Laser: Strong Performance on Acrylic and Organic Materials
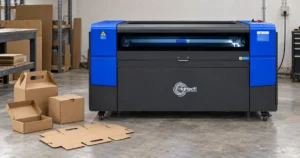
A CO2 laser commonly operates at approximately 10.6 µm. Acrylic, wood, MDF, compatible leather, fabric, paper, and selected plastics respond well to this wavelength. The technology can cut profiles, engrave text and graphics, and process a broad mix of substrates without physical tool contact.
read more: CO2 Laser for Cutting Acrylic
Beam Delivery and Maintenance
Fiber lasers use a solid-state source and fiber-optic beam delivery. CO2 systems use a gas-based source and an optical path that normally includes mirrors and lenses. The CO2 design can require more routine optical cleaning and alignment, while fiber systems generally have fewer optical components in the beam-delivery path. Maintenance requirements still vary by machine design, working environment, extraction system, and daily operating hours.
Fiber Laser vs CO2 Laser for Metal Cutting
For most new metal-cutting investments, fiber technology is the stronger choice. It is designed for fast processing of metal sheet and plate, supports reflective materials more effectively, and usually offers lower optical maintenance. CO2 machines may remain productive in established lines, but businesses buying new equipment should compare cost per finished part rather than relying only on purchase price or rated laser power.
Can a CO2 Laser Cut Metal?
Yes, an industrial CO2 laser equipped for metal cutting can process metals such as steel. This requires a suitable source, cutting head, assist-gas system, and process configuration. It does not mean that a workshop CO2 engraver intended for acrylic and wood can cut metal sheet.
For a fiber vs CO2 laser cutting comparison, compare machines designed for the same metal, thickness, and output requirement. A low-power non-metal engraver and an industrial sheet-cutting system are not equivalent alternatives.
Fiber Laser vs CO2 for Stainless Steel Precision
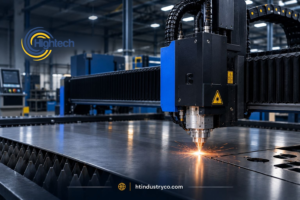
Fiber lasers can focus to a small spot, which supports narrow kerfs, small holes, fine contours, and repeatable dimensions on thin and medium-gauge stainless steel and aluminum. These capabilities are valuable for enclosures, machine parts, decorative panels, kitchen equipment, mounting plates, metal letters, and architectural components. Assist-gas selection, nozzle condition, focal position, machine motion, and cutting parameters still determine the final edge quality.
Specify the required dimensional tolerance and inspect holes, corners, burrs, roughness, and flatness on representative samples. A narrow kerf is not, by itself, proof of dimensional accuracy. Include any cleaning or finishing needed before bending, welding, or assembly.
Copper, Brass, and Other Reflective Metals
Copper and brass reflect the CO2 wavelength strongly, which makes bare reflective metals difficult and potentially risky for many CO2 systems. Fiber machines designed for these materials are the practical option for direct cutting and marking. Buyers should nevertheless confirm that the selected machine, source, cutting head, and process settings are approved for the exact metal grade and thickness.
Thin Sheet, Medium Plate, and Thick Material
Fiber lasers often provide a strong productivity advantage on thin and medium sheet. However, rapid-traverse speed is not cutting speed, and cutting speed is not the same as completed parts per hour.
Older CO2 processes were historically valued for smooth edges on some thick mild-steel applications. Modern high-power fiber systems have narrowed many of those differences, so sample cuts should be evaluated using the buyer’s real material grades, thicknesses, gas supply, and quality requirements.
There is no universal thickness at which CO2 becomes the better choice. Compare complete batches, including piercing, contour complexity, loading, unloading, rejected parts, and secondary finishing.
Fiber Laser vs CO2 Laser Engraving and Marking
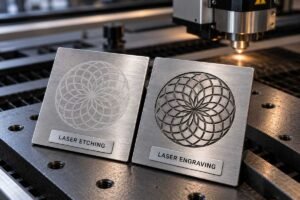
For direct marking and engraving on bare stainless steel, aluminum, brass, and similar metals, a suitably configured fiber marking system is generally the better starting point. Engraving removes material; other marking processes may alter surface appearance without producing a recessed mark. Required depth and contrast should be specified separately.
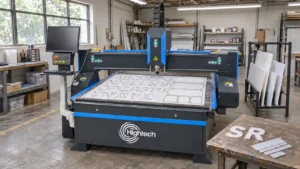
Hightech’s fiber marking machine is an option for text and graphics on compatible metals. Evaluate the actual substrate, finish, artwork, and marking requirements before selecting the configuration. Do not assume that a sheet-cutting machine provides the same workflow as a dedicated marker.
CO2 engraving is useful for wood, acrylic, compatible leather, and other non-metals. It can also mark suitable coated or anodized metals, or create marks on some bare metals using a compatible marking compound. These processes should not be confused with deep engraving into bare metal or cutting through a metal sheet.
For acrylic engraving, cast acrylic generally produces a frosted appearance, while extruded acrylic reacts differently and is often chosen for smooth cut edges. For a small engraving business, choose according to the products being sold: metal tags and industrial identification favor fiber; acrylic awards, wood gifts, and compatible leather products favor CO2.
Does Fiber Laser Harden Metal Edges?
Laser cutting can create a heat-affected zone, but it does not always harden the edge. Hardness changes depend on the alloy, its initial condition, and the heating and cooling cycle. Both fiber and CO2 cutting are thermal processes.
Stainless steel should not be treated as one uniform material. Discoloration, burrs, edge roughness, and hardness are different properties; the appearance of the edge does not establish its hardness.
Where subsequent forming, machining, welding, or corrosion performance is critical, agree the acceptance criteria and test representative cut samples. A narrow heat-affected zone does not mean there is no thermal effect. Laser surface hardening is a separate process from cutting.
Fiber Laser vs CO2 Laser for Signage
Signage is a mixed-material industry, so the correct laser depends on the shop’s product mix. Acrylic faces, illuminated channel letters, wood signs, stainless-steel letters, aluminum panels, brass plaques, and industrial labels do not respond to the same wavelength. The most profitable machine is the one that matches the material categories the shop processes every day.
Acrylic Faces and Illuminated Channel Letters: Why CO2 Wins
CO2 lasers are the practical choice for acrylic sign components. With suitable material and settings, they can leave smooth cut edges and reduce secondary finishing. Extruded acrylic is particularly useful when a glossy cut edge is the priority; cast acrylic is commonly selected for frosted engraving. Check the required appearance on the actual sheet grade.
A fiber laser is not a substitute for this workflow because acrylic does not absorb the fiber wavelength in the same useful way. Increasing fiber-laser power does not turn it into an acrylic-cutting system. Shops that rely on channel-letter faces, acrylic logos, display components, or illuminated panels should treat a CO2 machine as a core production tool.
Wood, MDF, Plastics, and Layered Signage
CO2 machines also support cutting and engraving on wood, MDF, plywood, compatible laminates, leather, fabric, paper, and selected plastics. A sign shop can use one system for rustic storefront signs, dimensional letters, layered plaques, decorative panels, templates, and customized graphics. Material safety should always be confirmed before processing coated, laminated, or chemically treated products, because some materials can release hazardous fumes or damage equipment.
For CO2 vs fiber laser leather cutting, CO2 is generally the appropriate starting point, provided the leather and its treatments are approved for laser processing. Synthetic leather may contain PVC and must not be assumed safe. Foam also needs formulation-specific approval; a material name alone does not confirm suitability.
Metal Storefront Letters, Aluminum Panels, and Brass Plaques: Why Fiber Wins
When the work moves to stainless steel, aluminum, brass, or copper, the advantage shifts to fiber. Fiber lasers can cut metal letters, logos, mounting plates, decorative panels, nameplates, and structural sign components directly. They also maintain fine detail on small text and intricate shapes, which is valuable for plaques, directories, industrial signage, and dimensional metal branding.
The speed advantage becomes commercially important on repeat production. Faster metal processing can increase the number of jobs completed per shift, while consistent kerf width and repeatable dimensions can reduce fitting and finishing time. Thin signage metal can be sensitive to vibration and heat, so machine rigidity, motion control, nesting, assist gas, and parameter setup remain important.
Best Laser for Common Sign Materials
Sign material or product | Recommended technology | Reason |
|---|---|---|
Cast-acrylic letters and faces | CO2 laser | Clean cutting and a glossy edge suitable for illuminated signage |
| Wood, MDF, plywood and layered plaques | CO2 laser | Cuts and engraves organic materials effectively |
| Fabric, paper and selected plastics | CO2 laser | Broad non-metal material compatibility |
| Stainless-steel storefront letters | Fiber laser | Fast metal cutting with fine detail and repeatability |
| Aluminum panels and mounting plates | Fiber laser | Efficient absorption and accurate metal processing |
| Brass plaques and metal nameplates | Fiber laser | Direct cutting or marking with permanent detail |
| Mixed acrylic and metal signage | Both, or phased investment | Each technology handles a different part of the workflow |
How a Mixed-Material Sign Shop Should Invest
A new sign shop does not always need to purchase both technologies immediately. The first machine should match the material group that produces the largest share of current and near-term revenue:
- Mostly acrylic faces, channel letters, wood, and display work: start with CO2.
- Mostly stainless-steel letters, aluminum components, plaques, and industrial signs: start with fiber.
- Mixed work with more non-metal demand: buy CO2 first and add fiber as metal orders grow.
- Mixed work with more metal demand: buy fiber first and add CO2 when acrylic and wood volume justifies it.
Outsourcing the smaller material category can be a sensible temporary strategy. Compare avoidable outsourcing costs and the contribution from additional orders with the full ownership and operating costs of a second machine. Revenue alone does not establish the return on investment.
Operating Cost, Maintenance, and ROI
Purchase price is only one part of the investment. A useful comparison includes electricity, assist gas, extraction, cooling, consumables, optics, planned maintenance, unplanned downtime, labor, and the value of jobs the machine makes possible.
Why Fiber Often Costs Less to Operate for Metal
Fiber laser sources generally provide higher electrical efficiency and require less optical-path maintenance than comparable CO2 metal-cutting systems. For a metal-focused operation running multiple shifts, the difference in electricity, optics, maintenance time, and throughput can have a major effect on cost per part. The actual savings depend on laser power, duty cycle, local energy prices, assist-gas consumption, and machine configuration.
Fiber does not mean maintenance-free. Cutting-head optics, nozzles, cooling, extraction, and the motion system still require attention. Likewise, CO2 source service varies between sealed tubes and other resonator designs; not every CO2 machine requires routine resonator-gas refilling.
Fiber Laser vs CO2 Laser Power Consumption
Wall-plug efficiency describes the proportion of electrical input converted into laser output. It is different from how much of that beam energy the workpiece absorbs, and different again from the electricity used by the entire production cell.
For a useful comparison, measure electricity over the same production job, including the laser, cooling, extraction, and relevant auxiliary equipment. Divide the energy used by the number of accepted parts to obtain kWh per finished part. Include idle periods and rework where they are part of the normal workflow.
Why CO2 Can Still Be the Better Business Purchase
A lower-cost machine that performs the shop’s core work is often a better investment than a more advanced machine that cannot process the required materials. For a business producing acrylic signs, wood products, engraved gifts, displays, or fabric components, CO2 technology may generate revenue immediately and eliminate manual finishing. Its higher maintenance needs should be included in the budget, but they do not outweigh the material advantage when non-metals are the main workload.
Fiber Laser vs CO2 Laser Cost
When comparing fiber laser vs CO2 laser cost, the purchase price is only one part of the decision. A CO2 laser may have a lower entry cost, especially for acrylic, wood, leather, paper, and mixed non-metal production. This makes it attractive for sign shops, engraving businesses, and workshops that need flexible non-metal processing.
A fiber laser cutting machine is usually more expensive at the beginning, especially when configured for industrial metal cutting. However, for metal-focused businesses, fiber lasers often deliver lower long-term cost per part because they cut metal sheets faster, require less optical alignment, and provide higher efficiency on stainless steel, mild steel, aluminum, brass, and copper.
So, why is it so expensive? The higher cost usually comes from the fiber laser source, cutting head, motion system, safety enclosure, automation options, gas system, and the precision required for high-power fiber lasers. For businesses working mainly with metal, that higher investment can be justified by faster throughput, lower maintenance, and better productivity.
In simple terms: choose CO2 when your revenue comes from non-metal materials, and choose fiber when your business depends on metal cutting, stainless steel precision, industrial fabrication, or high-volume sheet metal production.
Decision Matrix: Which Laser Suits Your Business?
Business profile | Primary materials | Recommended first machine | Reason |
|---|---|---|---|
| Industrial metal fabricator | Steel, stainless, aluminum, brass, copper | Fiber laser | Metal speed, reflective-metal capability and lower optical maintenance |
| Metal-sign producer | Metal letters, panels, plaques, mounting parts | Fiber laser | Detailed direct processing of thin signage metal |
| Acrylic and illuminated-sign shop | Acrylic, plastics, channel-letter faces | CO2 laser | Clean acrylic cutting and polished-looking edges |
| Wood and engraving business | Wood, MDF, leather, paper, fabric | CO2 laser | Broad organic-material cutting and engraving |
| Mixed sign shop, mostly non-metal | Acrylic and wood with occasional metal | CO2 first | Supports the dominant workload; outsource metal initially |
| Mixed sign shop, mostly metal | Metal with occasional acrylic or wood | Fiber first | Supports the dominant workload; outsource non-metal initially |
| Diversified, high-volume sign factory | Metal and non-metal in meaningful volume | Fiber + CO2 | Dedicated technologies improve quality and workflow for each material group |
Choose a Fiber Laser If...
- Most of your revenue comes from metal cutting, fabrication, or metal signage.
- You regularly process stainless steel, mild steel, aluminum, brass, or copper.
- Thin- and medium-sheet speed is important to throughput.
- You need direct metal marking, detailed logos, serial numbers, or nameplates—in which case, evaluate a dedicated marking machine.
- Lower optical maintenance and predictable uptime are purchasing priorities.
Choose a CO2 Laser If...
- Your main materials are acrylic, wood, MDF, leather, fabric, paper, or selected plastics.
- You produce illuminated signs, channel-letter faces, displays, or engraved non-metal products.
- A glossy acrylic edge and detailed wood engraving are central to product quality.
- You need one machine for a broad variety of non-metal substrates.
- The lower entry cost aligns better with your current production volume and sales pipeline.
Find the Right Machine for Your Application
Frequently Asked Questions
What is the difference between a CO2 laser and a fiber laser?
They use different laser sources and wavelengths. Common industrial fiber systems operate near 1.06–1.07 µm, while many CO2 systems operate near 10.6 µm. This affects material response: fiber is generally preferred for metal processing, while CO2 suits acrylic, wood, and many other non-metals.
Which laser is better for stainless steel?
A fiber cutting machine is generally the better starting point for new stainless-steel sheet production. For text, logos, or identification on finished parts, evaluate a fiber marking machine. Final quality depends on the grade, thickness, required operation, and process settings.
Can a fiber laser cut acrylic or wood?
Not as a practical production process. Acrylic, wood, and similar non-metals respond far better to a CO2 laser. A sign shop producing acrylic faces, wood signs, or engraved organic materials should use CO2 technology.
Which laser is best for acrylic signs and channel letters?
A CO2 laser is the appropriate choice for cutting acrylic sign faces. Select the acrylic type and settings according to the desired edge finish or engraved appearance, and test the actual stock before production.
Which laser is best for metal storefront letters and brass plaques?
A fiber laser is the stronger choice. It can cut or mark stainless steel, aluminum, brass, and other metals directly while maintaining fine text, logos, and repeatable dimensions.
Can one machine handle every sign material?
No single laser performs equally well on metals and non-metals. A mixed-material shop can begin with the machine that matches its dominant workload, outsource the smaller category, and add the second technology when order volume justifies it.
Does a fiber laser have lower maintenance?
Is fiber always more profitable than CO2?
No. Profitability depends on material mix and sales demand. Fiber is usually more economical for metal-heavy production, while CO2 can be the more profitable purchase for acrylic, wood, and other non-metal products.
How should I compare ROI?
Use your own job prices, expected monthly volume, gross margin, energy and gas costs, maintenance budget, finance cost, and the value of work currently outsourced. Compare conservative and realistic scenarios before purchasing.
Latest contents
Prefer a callback? Share your details and requirements below.
Your details will only be used to respond to this request.